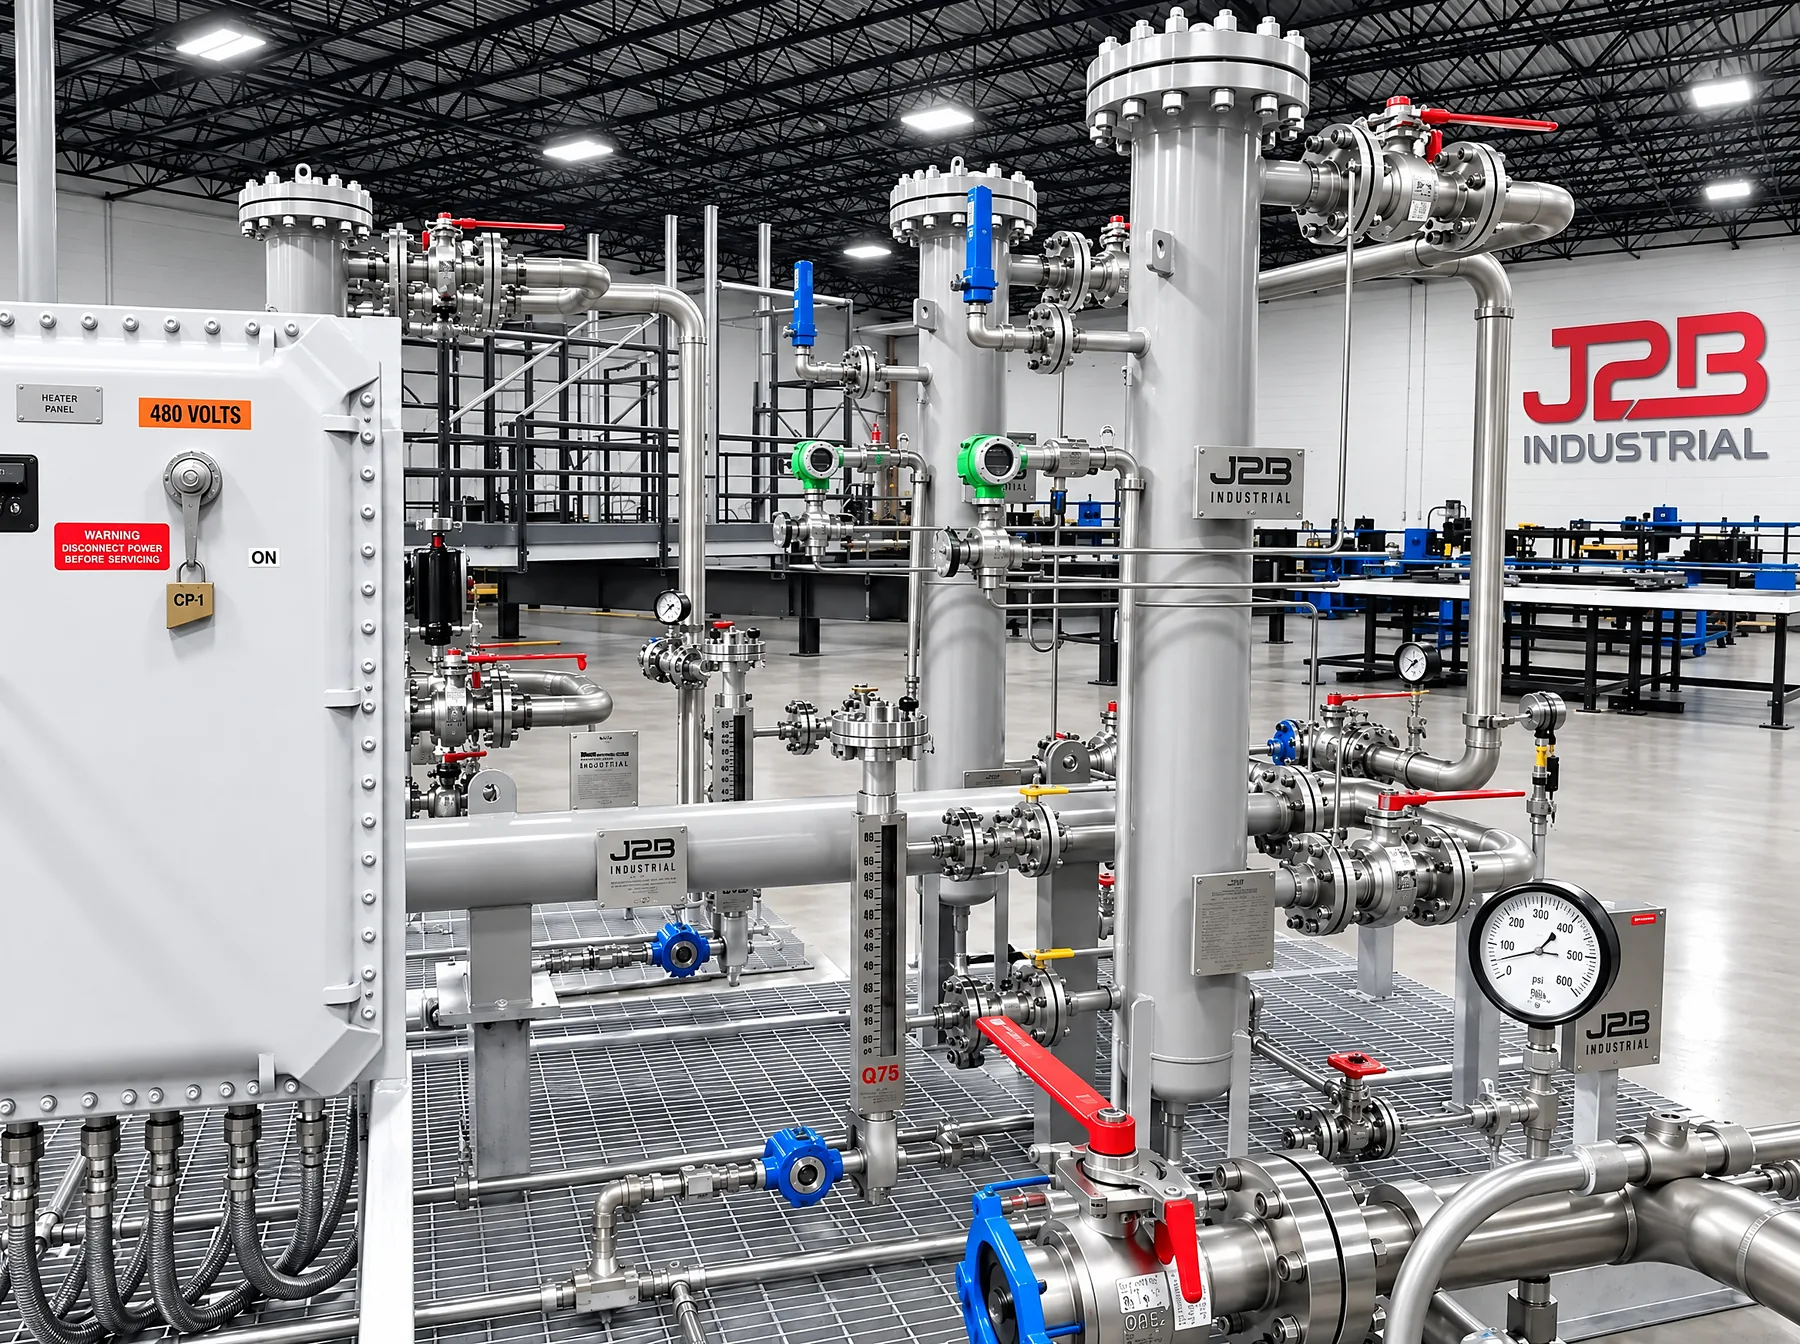
A Factory Acceptance Test is the last point where a problem is cheap to fix. Once a skid ships, every defect found costs field labor, schedule and often a turbine outage. A well-scoped FAT proves the package does what the design says before it leaves the shop.
Purpose
The FAT confirms three things: the unit was built to the released design, it holds pressure and is safe, and its controls and shutdowns behave as the cause and effect matrix requires. It is run to a written procedure agreed with the customer in advance, with witness points identified in the inspection and test plan.
Before the FAT
- Hydrostatic or pneumatic testing complete and recorded
- Required nondestructive examination complete and accepted
- Instrument installation checked against the instrument index
- Wiring, terminations and grounding inspected; point-to-point checks complete
- Control program loaded at the released revision
Test scope
| Area | What is demonstrated |
|---|---|
| Documentation | As-built drawings, material records, weld records and test records are complete for the serial number |
| Dimensional | Interface connections, nozzle locations and lifting points match the drawings |
| Instruments | Tag, range and calibration verified; loop checks from field device to PLC |
| Control functions | Heater control, level control and pressure control respond as designed on simulated inputs |
| Alarms and shutdowns | Every cause in the cause and effect matrix produces the required effect; shutdown valves stroke and reset correctly |
| Communications | Signals to the plant or turbine control system are mapped and verified |
| Visual and preservation | Coatings, labeling, tagging and shipping preservation are complete |
Closing the FAT
Findings go on a punch list with owners and dates. The unit is released only when punch items are closed or formally accepted as deviations, and the signed FAT report joins the unit's Manufacturing Record Book. On fleet programs the first article's FAT is usually the most extensive; later units repeat the same procedure so results can be compared unit to unit.