Quality
Work is executed to the applicable project requirements, specifications, governing codes and OEM requirements, and every step is recorded against the unit's serial number.
Built to the governing code
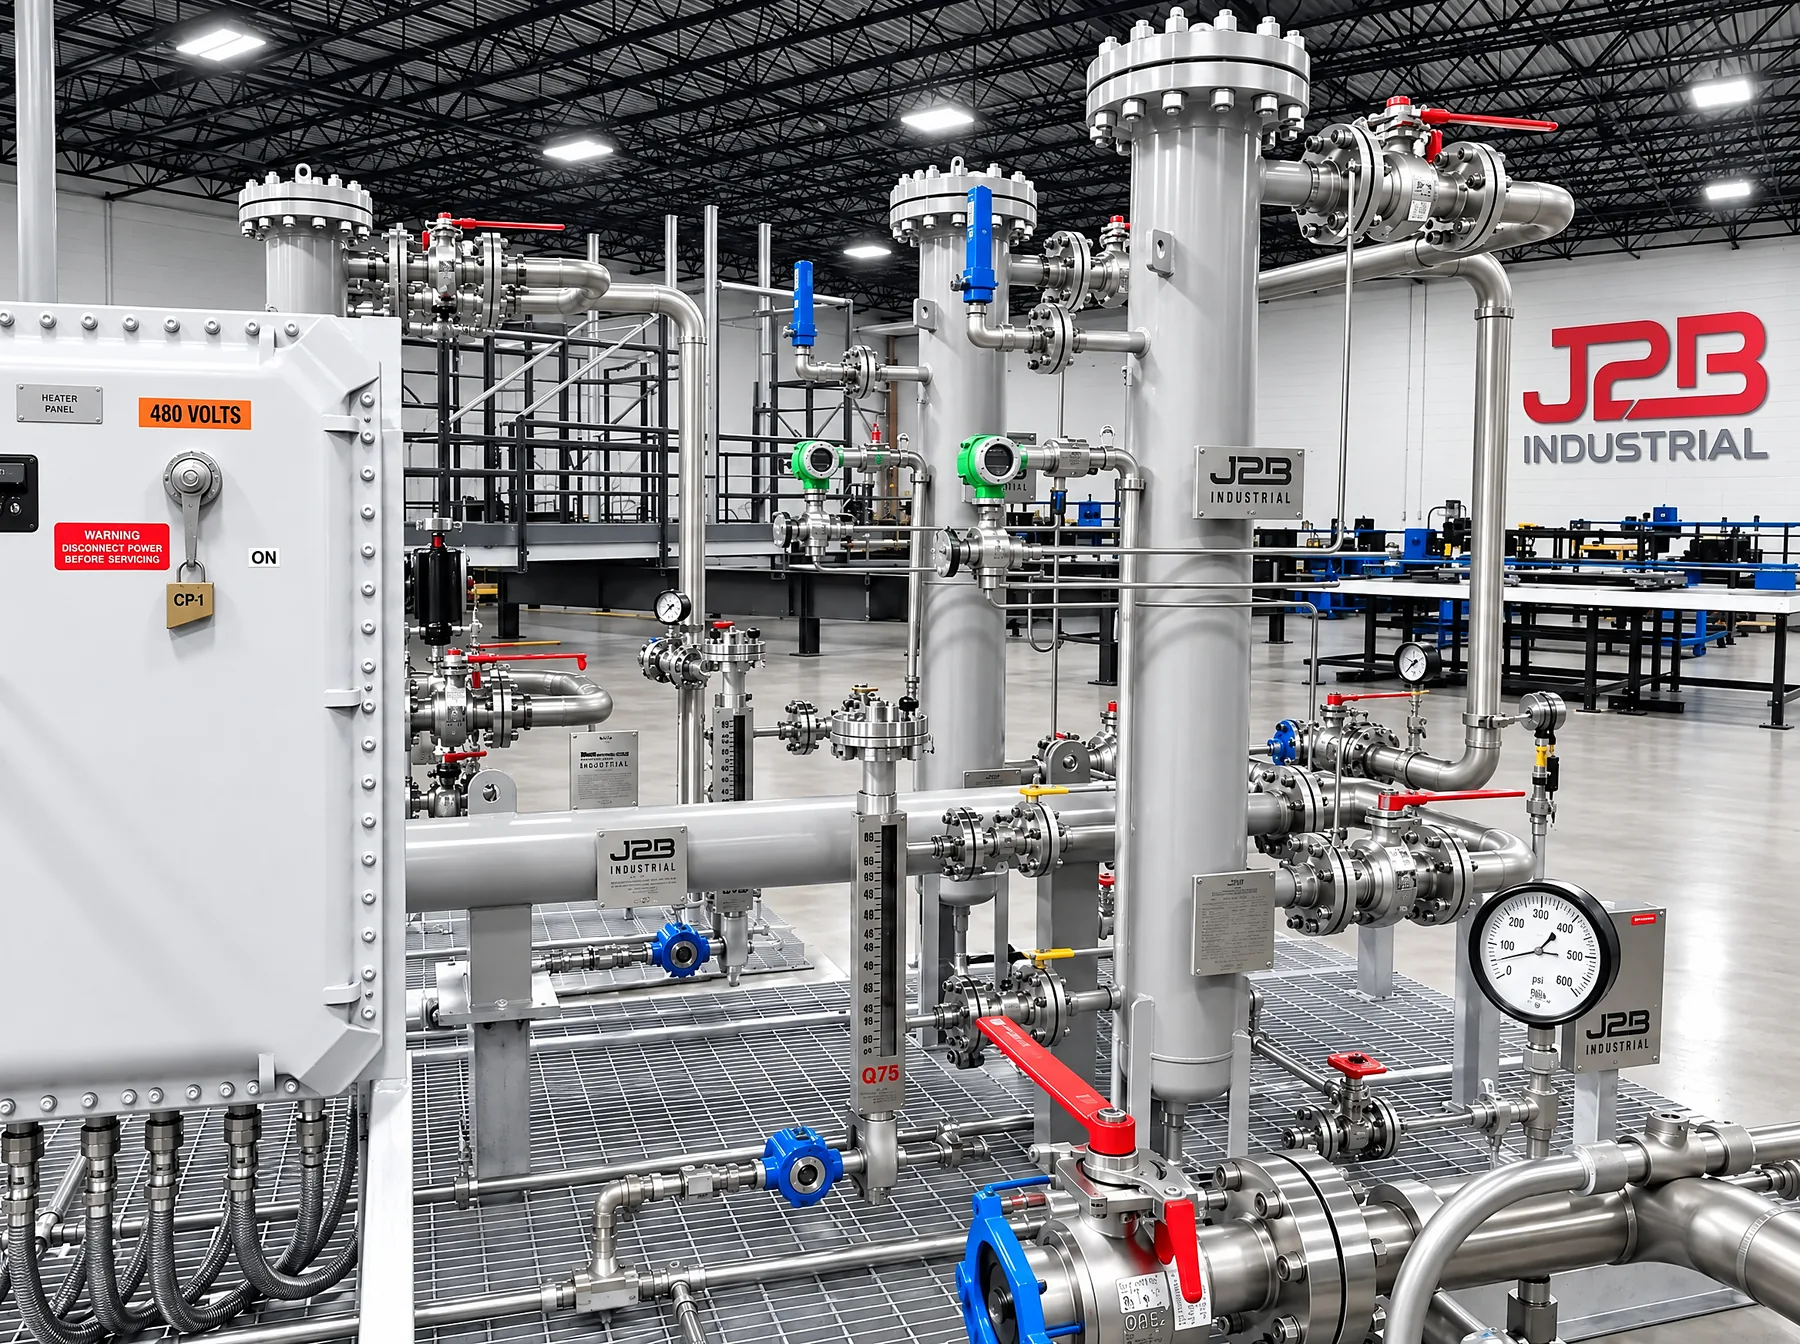
J2B designs and manufactures each system to the applicable governing code and project basis. The service, the installation and the owner's requirements determine which code governs.
Quality built into every unit
From qualified procedures to the turnover package, each unit carries the record of how it was built and tested.
Qualified welding
Qualified welding procedures, with each joint assigned a welder qualified to its procedure.
Material traceability
Pressure-retaining material traced to its mill test report and heat number.
Inspection
Fit-up, dimensional and in-process inspection at defined points in the build.
NDE where required
Nondestructive examination to the extent the code and the project require.
Pressure and functional testing
Hydrostatic or pneumatic testing, loop checks and functional tests.
Factory Acceptance Testing
FAT to an approved procedure, witnessed as the customer specifies.
Documentation and turnover
A Manufacturing Record Book and turnover package for every unit.
Hazardous-area construction
Class I, Division 1 and Class I, Division 2 construction as the project requires.
Hazardous-area construction
Electrical construction for Class I, Division 1 and Class I, Division 2 locations, depending on project requirements. The project's area classification sets the enclosures, instruments, wiring methods and seals.
| Classification | Typical condition |
|---|---|
| Class I, Division 1 | Locations where ignitable concentrations of flammable gases or vapors can exist under normal operating conditions |
| Class I, Division 2 | Locations where flammable gases or vapors are normally confined and can escape only under abnormal conditions |
Materials for service life
Process piping, fittings, flanges, valves and instrumentation tubing in stainless steel, including 316 stainless where specified or required. Structural skid frames are typically hot-dip galvanized unless the customer specification requires another material or coating.
From material receipt to shipping release
Each gate produces a record tied to the serial number. Hold points, marked in red, stop production until the inspection is complete and accepted.
Material receipt
ReceivingIncoming material checked against the purchase order, quantity and condition.
Material verification
InspectionGrade, size, schedule and markings verified against the specification.
MTR / heat traceability
Hold pointMill test reports reviewed; heat numbers transferred and logged for pressure-retaining material.
Controlled drawings
Document controlOnly released drawings at the current revision reach the floor.
WPS / qualified welding
QualificationEach joint assigned a qualified procedure and a welder qualified to it.
Fit-up inspection
InspectionAlignment, gap, bevel and dimensions checked before welding begins.
Welding
ProductionWelds made to the assigned WPS and recorded on the weld map by welder ID.
NDE
Hold pointNondestructive examination performed to the code and project extent.
Pressure testing
Hold pointHydrostatic or pneumatic test at the required pressure and hold time.
Instrument verification
InspectionInstruments checked against the index for tag, range, calibration and installation.
Electrical / controls verification
InspectionWiring, terminations, grounding and loop checks verified end to end.
FAT
Hold pointFactory Acceptance Test run to the approved procedure, witnessed as specified.
Manufacturing Record Book
Document controlAll records compiled and reviewed against the serial number.
Shipping release
Hold pointFinal inspection, preservation and release authorization before the unit leaves.
- Model
- Fuel gas conditioning skid
- Serial no.
- Assigned at start of build
- Design basis
- Released drawing revision
- Materials
- Traced to MTR and heat number
- Testing
- Hydrostatic and FAT, signed
Stainless nameplate, one per unit
The Manufacturing Record Book
Issued per serial number: the complete quality history of the unit.
- Certificate of conformance
- As-built drawings at released revision
- Material test reports and heat log
- Weld map, WPS, PQR and welder qualifications
- Fit-up and dimensional reports
- NDE reports
- Pressure test records
- Instrument and calibration data
- Electrical and loop check records
- FAT report and punch list closure
- Deviations and approved changes
- Shipping release and preservation
System controls
| Contract and specification review | Requirements captured before engineering begins |
|---|---|
| Supplier qualification | Approved sources for pressure parts and critical components |
| Inspection and test plans | Hold and witness points agreed with the customer |
| Dimensional verification | Critical interfaces checked before assembly and before shipment |
| Nonconformance control | Deviations recorded, dispositioned and closed |
| Calibrated equipment | Gauges and test instruments under calibration control |
| Functional testing | Controls, shutdowns and alarms proven before FAT |
| Final documentation | Turnover package complete at shipping release |
Let's build your next program.
Whether you are developing a single installation or planning a fleet deployment, J2B Industrial can work with your team to develop an engineered, manufacturable solution and establish the production capacity required to support your schedule.
Or call (904) 574-8919 · sales@j2bindustrial.com
Design basis or specification ready? Send your design basis